A Guide to Material Handling Equipment and Systems
Material handling equipment and systems are used to move, store, protect, control, and organize materials throughout industrial and commercial facilities.
They can handle raw materials, components, finished products, containers, pallets, and other loads at different stages of production and distribution.
These systems range from simple manual equipment to highly automated solutions. The appropriate configuration depends on material characteristics, load capacity, facility layout, movement distance, storage requirements, and operational conditions.
What Is Material Handling Equipment?
Material handling equipment refers to mechanical, electrical, or automated equipment used to move and manage materials within a facility or between designated handling points.
The equipment can perform several functions, including:
- Lifting and lowering
- Horizontal transportation
- Loading and unloading
- Stacking and retrieving
- Sorting and routing
- Storage and retrieval
- Positioning
- Order movement
- Pallet handling
Material handling systems can combine several types of equipment to create an integrated movement and storage process.
Main Types of Material Handling Equipment
Material handling equipment can generally be grouped according to its primary function.
| Equipment Type | Main Function | Common Applications |
|---|---|---|
| Conveyors | Continuous material movement | Production lines and warehouses |
| Forklifts | Lifting and transporting loads | Warehouses and factories |
| Pallet Jacks | Moving palletized loads | Storage and distribution areas |
| Cranes | Lifting heavy loads | Manufacturing and construction |
| Hoists | Vertical lifting | Workshops and production areas |
| Automated Guided Vehicles | Automated transportation | Factories and warehouses |
| Robotic Systems | Picking and movement | Automated facilities |
| Storage Systems | Organizing materials | Warehouses |
| Sortation Systems | Routing products | Distribution facilities |
| Dock Equipment | Loading and unloading | Shipping areas |
Conveyors
Conveyors are continuous or semi-continuous transportation systems that move materials along a defined path.
Belt Conveyors
Belt conveyors use a continuous belt supported by rollers or a conveying surface. They can transport cartons, packages, bulk materials, and components.
Roller Conveyors
Roller conveyors use a series of rollers to move products. Powered and gravity-based versions are used for different material movement requirements.
Chain Conveyors
Chain conveyors use one or more chains to transport pallets, containers, and heavy products. They are often used where loads require strong supporting surfaces.
Screw Conveyors
Screw conveyors use a rotating helical element to move bulk materials. They can handle materials such as powders, granules, and other loose products.
Forklifts and Industrial Trucks
Forklifts are mobile equipment used to lift and transport palletized or individual loads. Their forks move underneath a load, allowing the mast and lifting mechanism to raise it to a required height.
Different configurations are designed for different operating environments, including:
- Counterbalance forklifts
- Reach trucks
- Pallet trucks
- Order pickers
- Narrow-aisle trucks
- Rough-terrain forklifts
Selection depends on load weight, lifting height, aisle width, floor conditions, and operating environment.
Cranes and Hoists
Cranes and hoists are used when loads need to be lifted vertically and positioned across a defined area.
Overhead Cranes
Overhead cranes operate along elevated runways and can move heavy loads across manufacturing facilities, workshops, and industrial plants.
Gantry Cranes
Gantry cranes are supported by legs and can operate on ground-level rails or tracks. They are used in warehouses, yards, fabrication areas, and other open spaces.
Jib Cranes
Jib cranes use a horizontal or angled boom that rotates around a fixed support. They are useful for localized lifting around workstations.
Hoists
Hoists provide controlled vertical lifting and lowering. They can be integrated with overhead cranes, gantry structures, workstation systems, or other lifting equipment.
Automated Material Handling Systems
Automation has become an important part of modern material movement and storage. Automated equipment can reduce manual handling requirements and coordinate repetitive movement tasks.
Common technologies include:
- Automated guided vehicles
- Autonomous mobile robots
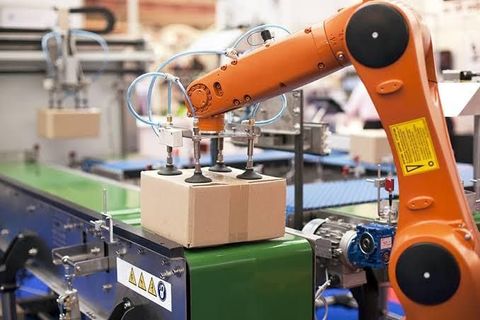
- Robotic arms
- Automated storage and retrieval systems
- Conveyor control systems
- Automated sortation equipment
- Warehouse control software
- Machine vision systems
Automated systems can use sensors, programmable controllers, navigation technologies, and software to coordinate material movement.
Automated Guided Vehicles and Mobile Robots
Automated guided vehicles, or AGVs, are mobile machines that transport materials along predefined or digitally controlled routes.
Autonomous mobile robots, or AMRs, can navigate dynamic environments using sensors and mapping technologies. They may transport bins, totes, cartons, pallets, or other materials between designated locations.
| Technology | Navigation Approach | Typical Use |
|---|---|---|
| AGV | Defined routes or guidance systems | Repetitive transportation |
| AMR | Sensor-based navigation | Dynamic warehouse movement |
| Robotic Arm | Programmed movement | Picking and positioning |
| Automated Conveyor | Fixed path | Continuous transportation |
| AS/RS | Automated storage and retrieval | High-density storage |
Storage and Retrieval Equipment
Storage systems organize materials while making them accessible for retrieval.
Pallet Racking
Pallet racks provide structured storage locations for palletized materials. Configurations can vary according to warehouse height, load characteristics, and accessibility requirements.
Automated Storage and Retrieval Systems
Automated storage and retrieval systems use mechanical equipment and software to place and retrieve loads from storage locations.
Vertical Lift Systems
Vertical lift equipment uses vertical storage space to organize smaller components, parts, and inventory containers.
Shelving Systems
Shelving systems are commonly used for smaller materials and manually accessible inventory.
Sortation Systems
Sortation systems direct materials toward different destinations based on predefined criteria. They are commonly used in distribution centers and order-processing environments.
Sensors can identify packages using barcodes, RFID technology, dimensions, or other information. Control software then determines the appropriate routing path.
Dock and Loading Equipment
Material handling also includes equipment used at loading and unloading areas.
Examples include:
- Dock levelers
- Dock shelters
- Loading ramps
- Pallet handling equipment
- Lift tables
- Vehicle restraints
- Conveyor loading systems
These systems help bridge differences between warehouse floors and vehicle platforms while supporting controlled material movement.
Main Components of Material Handling Systems
Integrated systems can contain mechanical, electrical, and digital components.
| Component | Function |
|---|---|
| Motors | Provide mechanical movement |
| Gearboxes | Transfer and modify rotational motion |
| Sensors | Detect position, movement, or objects |
| Controllers | Coordinate equipment operation |
| Conveyors | Transport materials |
| Lifting mechanisms | Raise and lower loads |
| Frames | Provide structural support |
| Control panels | Manage electrical systems |
| Software | Coordinate automated operations |
| Safety devices | Help control operational hazards |
How Material Handling Systems Work
A material handling system generally follows a sequence based on the facility's workflow.
1. Material Receiving
Materials enter the facility through receiving areas. Items may be unloaded manually or through powered equipment.
2. Identification
Barcodes, RFID tags, sensors, or other identification technologies can be used to identify materials and determine their destination.
3. Transportation
Conveyors, forklifts, cranes, mobile robots, or other equipment move materials between locations.
4. Storage
Materials are placed into racks, shelves, bins, automated storage systems, or designated floor locations.
5. Retrieval
When materials are required, workers or automated systems retrieve them from storage.
6. Processing or Order Movement
Materials may move to production lines, assembly stations, packing areas, or order fulfillment zones.
7. Shipping
Finished products are transported to staging and loading areas before leaving the facility.
Factors Affecting Equipment Selection
The appropriate material handling system depends on multiple factors.
Material Characteristics
Weight, size, shape, fragility, temperature, surface properties, and packaging can influence equipment selection.
Load Capacity
Equipment must be appropriately rated for the maximum expected load. Overloading can create mechanical and safety hazards.
Travel Distance
Short-distance workstation movement may require different equipment from long-distance warehouse transportation.
Facility Layout
Aisle width, ceiling height, floor conditions, storage height, production areas, and loading zones all influence system design.
Movement Frequency
High-volume operations may benefit from continuous conveyors or automated transportation systems, while intermittent movement may suit mobile equipment.
Environmental Conditions
Dust, moisture, temperature, chemicals, outdoor exposure, and other environmental factors can affect equipment selection and maintenance.
Material Handling Automation and Digital Systems
Modern material handling systems can integrate operational data with warehouse and production software.
Warehouse management systems can track inventory locations and movement. Warehouse control systems can coordinate conveyors, sortation equipment, automated storage systems, and robotic devices.
Sensors can provide information about equipment status, load position, movement, and operating conditions. This information can support monitoring and maintenance planning.
Safety Considerations
Material handling equipment can involve moving machinery, elevated loads, vehicle traffic, and electrical systems. Appropriate safety procedures are therefore essential.
Important practices include:
- Following equipment operating instructions
- Keeping loads within rated capacity
- Maintaining clear travel paths
- Separating pedestrians and vehicles where appropriate
- Inspecting lifting attachments
- Using appropriate personal protective equipment
- Training operators
- Maintaining emergency stopping systems
- Inspecting equipment regularly
- Following applicable workplace regulations
Suspended loads should not be positioned over personnel, and damaged equipment should be removed from operation until appropriately inspected.
Maintenance Requirements
Regular maintenance helps identify wear, damage, and developing equipment problems.
Typical activities can include:
- Inspecting belts and chains
- Checking rollers and bearings
- Examining lifting components
- Testing brakes
- Inspecting electrical connections
- Checking sensors
- Lubricating applicable components
- Inspecting safety devices
- Reviewing control systems
- Cleaning equipment
- Recording maintenance activities
Maintenance intervals depend on equipment design, operating frequency, load conditions, and manufacturer recommendations.
Benefits of Integrated Material Handling Systems
A coordinated system can improve the organization of material movement within a facility.
Potential operational improvements include:
- More consistent material flow
- Better use of storage space
- Reduced unnecessary movement
- Improved inventory visibility
- More organized workflows
- Support for repetitive handling tasks
- Better coordination between storage and production
- Improved tracking of materials
The actual results depend on equipment configuration, facility design, operating procedures, and system management.
Frequently Asked Questions
What is material handling equipment?
Material handling equipment includes machines and systems used to move, lift, store, position, protect, and manage materials within industrial, warehouse, and commercial facilities.
What are the main types of material handling equipment?
Common types include conveyors, forklifts, pallet jacks, cranes, hoists, automated guided vehicles, mobile robots, storage systems, sortation systems, and dock equipment.
What is automated material handling?
Automated material handling uses technologies such as conveyors, robots, AGVs, AMRs, sensors, controllers, and software to perform or coordinate material movement with reduced manual intervention.
How is material handling equipment selected?
Selection depends on load characteristics, capacity, travel distance, facility layout, movement frequency, storage requirements, environmental conditions, and safety requirements.
Why is maintenance important for material handling equipment?
Maintenance helps identify component wear, mechanical problems, electrical faults, and safety issues. Regular inspections can support reliable equipment operation and reduce unexpected interruptions.
Conclusion
Material handling equipment and systems form an important part of warehouses, manufacturing plants, distribution centers, and other industrial facilities. They range from simple pallet handling equipment and conveyors to cranes, automated storage systems, robotic equipment, and autonomous mobile robots.
Effective system planning requires consideration of materials, load capacity, facility layout, travel requirements, storage conditions, automation needs, safety, and maintenance. As facilities adopt more digital and automated technologies, material handling systems are increasingly connected through sensors, controllers, software, and data-driven monitoring.

Related Post...
Rotary Cartridge Filling: An Overview of Filling Systems and Applications
Updated: September 26, 2026
Read More
Precision Dosing Equipment: An Overview of Accurate Material Measurement
Updated: September 26, 2026
Read More